Stock code
839391
The Cornerstone of Furnaces: How Are Refractory Bricks Produced
Release time:
2026-10-23
Author:
Source:
A furnace lining can fail even when every brick is built from the "right" chemistry. Uneven compaction, the wrong bonding system, out-of-tolerance dimensions, or a grade placed in a zone it was never designed for will all shorten campaign life—regardless of what the headline alumina or magnesia number says.
So how are refractory bricks produced, and which steps actually decide whether a brick survives service? The standard manufacturing route for shaped refractories is:
1. Raw-material preparation – crushing, grinding, screening, and where needed calcining.
2. Batching – weighing aggregates, fines, binders, and additives to the exact recipe.
3. Mixing – distributing the binder and matrix evenly into a homogeneous batch.
4. Forming – almost always pressing, which gives the brick its shape and green density.
5. Drying – removing free and residual moisture before heat treatment.
6. Firing – the high-temperature kiln stage that develops a ceramic bond (for fired grades only).
7. Finishing and inspection – checking, grinding to size, and releasing against agreed criteria.
Not every brick follows every step. Unfired and carbon-bonded shapes skip the kiln, and fused refractories take an entirely different melting-and-casting route. This guide walks the line in order and, at each stage, points out what you as a buyer should verify. At Jinheng Refractory (JHR) (JinXin HengTuo Advanced Materials), shaped bricks are supplied together with lining design, installation guidance, service support, and technical assistance—because a brick only performs when the product, the lining design, and the furnace duty are engineered as one system.

Refractory Bricks Start with Furnace Duty and Raw Materials
Material chemistry determines compatibility
Raw materials contain far more than the nominal Al₂O₃ or MgO value printed on a data sheet. Three things drive how a brick behaves at high temperature, against slag, and under mechanical stress:
• Mineralogical constitution – the actual phases present, not just the elemental oxide total.
• Impurity levels – low-melting oxides such as alkalis (K₂O, Na₂O) can depress hot strength and promote slag attack even at low concentrations.
• The bonding system – the ceramic, carbon, or chemical bond that holds the structure together.
Jinheng Refractory (JHR)'s shaped range covers the main ferrous duties: clay and high-alumina bricks for blast furnaces and hot-blast stoves; andalusite-, sillimanite-, and low-creep mullite-composite bricks for thermal-shock and creep resistance; magnesia-carbon (MgO-C) bricks for slag-zone steelmaking; and alumina–silicon-carbide–carbon (Al₂O₃-SiC-C) shapes for hot-metal and iron-contact wear.
Chemistry is always zone-specific. Tell your supplier about the slag, furnace atmosphere, temperature profile, and whether the brick contacts metal, gas, or both. A composition that is perfectly acceptable in a backing or safety lining may fail rapidly at the chemically aggressive hot face.
Particle preparation builds a controlled structure
Before any mixing, raw materials are crushed, ground, and separated into controlled size fractions; some are calcined or dried first. The resulting particle-size distribution governs how tightly the body packs:
• Coarse grains form the load-bearing skeleton and dominate thermal-shock behavior.
• Fines fill the gaps and form the matrix, controlling density, porosity, and slag penetration.
Get the grading wrong and no amount of pressing pressure will deliver the bulk density or strength the lining needs. This is why grain sizing is engineered to the target properties, not left to chance.
Refractory Bricks Gain Consistency through Mixing and Forming
Accurate batching keeps every brick on-formulation
To reproduce a proven laboratory recipe at full production scale, aggregates, fines, binders, and additives must be weighed in the exact batch ratios, shift after shift. Jinheng Refractory (JHR) uses automated batching for aggregates and powders with production data captured per batch. The buyer benefit is simple: traceability. If a question arises later, the issue can be traced back to a specific batch rather than an anonymous pile of bricks.
Binder distribution controls green quality
During mixing, the binder and fine matrix are distributed homogeneously through the batch. Where water or a liquid binder is added, the grains are wetted and the mix gains the plasticity needed for forming. The shaped-but-not-yet-fired piece is called a green brick—and it must hold its geometry after leaving the mold and be robust enough to handle, dry, and set down without cracking.
Pressed bricks need uniform compaction
Forming turns the prepared mix into the required shape, and pressing is essential for nearly all dense refractory shapes. But "it was pressed" is not a measure of quality. What matters is the pressing force, the number of strokes, and—above all—uniform density through the whole brick. A brick with soft zones will fire unevenly and is a pre-positioned crack in service.
Jinheng Refractory (JHR)'s hot-blast-stove low-creep high-alumina bricks are produced by high-pressure forming followed by high-temperature sintering in an automated workshop; semi-finished pieces are inspected, identified, and sorted—with rejects removed before they can travel further.
For purchasing, tie forming quality to measurable acceptance criteria up front: dimensional tolerances, visible defects (cracks, spalls, edge chipping), and agreed physical properties after the prescribed treatment.
Custom shapes make the lining fit
Brick geometry defines the joints and the way the lining carries load. Precision wedges, special shapes, and tightly defined interfaces remove most on-site cutting, speed up installation, and eliminate the weak points that field-cut bricks create. Jinheng Refractory (JHR) manufactures different sizes and shapes against your technical drawings and project requirements. For a non-standard shape, supply a dimensioned drawing showing tolerances, quantity, installation method, and mating/interface details.

Refractory Bricks Develop Their Bond during Heat Treatment
Drying and firing establish the bond
Drying removes moisture so the brick can safely enter the next thermal stage. The drying schedule is set by the body's properties and the brick's size—and a surface that feels dry does not mean internal moisture has escaped. Rushing this stage is a classic cause of bursting and cracking as trapped water turns to steam.
For fired products, the kiln cycle develops a ceramic bond. The bricks follow controlled heating, holding, and cooling curves in either a tunnel kiln (continuous) or a periodic (batch/shuttle) kiln, after which finishing steps bring them to the required dimensions and shape. Jinheng Refractory (JHR)'s platform covers automated drying, kiln-transfer logistics, centralized control, and flue-gas treatment for consistency and environmental compliance. One caveat for buyers: general plant capability is not the same as the grade-specific firing and release requirements for your order—confirm those before production.
Different bonding routes make different bricks
"Refractory brick" covers several bonding routes, and they do not all go through a kiln:
• Fired (ceramic-bonded) bricks – fired to form ceramic bonds between grains; the conventional route for most alumina, fireclay, and basic shapes.
• Unfired / carbon-bonded bricks – bonded with resin, pitch, or carbon and processed to their composition and bond type; common for MgO-C steelmaking bricks, with specific handling and heat-up requirements.
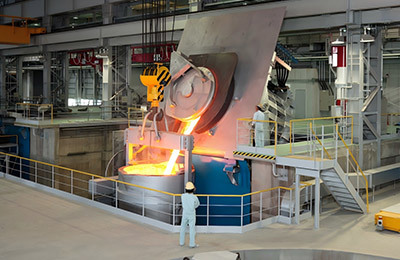
• Fused (fusion-cast) refractories – raw materials are melted in an electric furnace and cast into a mold, producing dense blocks such as fused AZS.
This is why a label that says simply "fired" can be almost meaningless for engineering. Ask instead for the bond type, the strength delivered for safe handling, the first heat-up/commissioning requirements, and any special-atmosphere or slow-ramp restrictions.
Refractory Bricks Must Pass Tests That Reflect Service
Density and porosity describe the structure
The two structural workhorses are bulk density (BD) and apparent porosity (AP). Apparent porosity is the accessible, interconnected porosity captured by the chosen test method—it is not the brick's total pore volume. Always compare numbers measured under the same standard (such as ASTM C20 / ISO 5017); values from different methods are not interchangeable.
Jinheng Refractory (JHR) tests incoming raw materials, the process itself, and the finished goods—rather than relying on a single end-of-line visual check. Capabilities include bulk-density and porosity determination, dimensional checks, chemical analysis, and microstructural inspection. When you receive results, request the test method, specimen conditions, sampling rules, and batch number so the data is traceable and comparable.
Above all, never compare typical catalog values against guaranteed acceptance limits. A typical value is a representative mid-range figure for reference; a guaranteed value is the contractual floor each delivered batch must meet. They serve different purposes.
Hot strength and thermal cycling separate the grades
Cold crushing strength (CCS) describes behavior under load at room temperature—a useful baseline, but it does not predict every high-temperature failure mode. A brick with strong CCS can still creep, soften, or spall in service. Ask for the tests that mirror the actual duty:
• Refractoriness-under-load (RUL) – deformation under load at temperature; critical for continuously loaded parts.
• Creep – long-term deformation at the relevant time, temperature, and load.
• Hot modulus of rupture (HMOR) – flexural strength at operating temperature.
• Thermal shock – resistance to rapid heating and cooling; always check the method (water vs. air quench, ΔT, cycle count), since numbers from different methods cannot be compared directly.
• Thermal expansion – for joint design and structural stress.
For hot-blast stoves, Jinheng Refractory (JHR) pairs low-creep high-alumina bricks with mullite-composite bricks matched to the different zones of the structure.
Refractory Brick Selection Should Connect Production with Installation
A lining is a system, not a single material. A dense working brick, an insulating backing brick, and a monolithic repair material each solve a different problem—chemical and mechanical wear at the hot face, heat loss through the shell, and fast in-service repair. Jinheng Refractory (JHR) develops linings by mapping thermal, chemical, and mechanical wear zone by zone, then selects compatible shaped, monolithic, insulating, and functional materials to suit. For blast-furnace and hot-blast-stove duties, explore our full shaped-refractory range.
When starting a project, work through this checklist with your supplier:
1. Provide furnace drawings, operating cycles, atmosphere, and slag chemistry.
2. Review previous wear history and the planned shutdown window.
3. Agree the material family, manufacturing route, and dimensions.
4. Agree the acceptance tests—and whether figures are typical or guaranteed.
5. Confirm traceability, packaging, and installation requirements.
Jinheng Refractory (JHR) supports the full sequence—material selection, lining design, manufacture, installation guidance, maintenance, and troubleshooting within the project scope—and links custom-product supply directly to these practical requirements. Lead time for custom shapes depends on tooling, dimensions, quantity, and testing, and is confirmed against the order.
FAQ
Q:What are the main refractory brick production stages?
Refractory bricks generally pass through raw-material preparation, batching, mixing, forming (pressing), drying, firing where the grade requires it, and finishing/inspection. The exact route depends on composition and bonding system; fused refractories instead follow a melting-and-casting process.
Q:Are all refractory bricks fired in a kiln?
No. Processing is determined by the bonding system. Conventional fired products develop a ceramic bond during kiln firing, while carbon-bonded and other unfired refractories are processed differently. Fused refractories are melted and cast. Confirm the processing route and first heat-up schedule with your supplier for the specific grade.
Q:How do dense refractory bricks differ from insulating fire bricks?
Dense refractory bricks are used at the working lining where strength and resistance to slag and metal penetration are needed. Insulating fire bricks are engineered around high porosity to reduce heat transfer and energy loss, so they are not placed in direct, aggressive contact with slag or molten metal. Chemical attack and mechanical duty decide the choice—temperature rating alone does not make the two interchangeable.
Q:Which refractory brick test results should buyers request?
Ask for chemistry, dimensions, bulk density, and apparent porosity, together with the relevant strength data. Add refractoriness-under-load, creep, thermal-shock, or compatibility data where the duty calls for it. Request the test standard and batch traceability, and agree specific acceptance criteria for your grade before production.
Q:Can refractory bricks be made to custom drawings?
Yes. Bricks can be tailored in shape, dimensions, and composition to project requirements. Provide dimensioned drawings with tolerances, the required quantity, and the intended operating conditions; Jinheng Refractory (JHR) will assess manufacturability and confirm a production schedule for the order.
Related Blog
2026-09-23
Contact Us
WhatsApp : +86 19143919677
Mobile / Wechat: +86 19143919677
E-mail: biting@jzjxht.com
Address: No. 688, Guangxing Road Boai County, Jiaozuo City, Henan Province
Copyright © Jiaozuo Jinxin Hengtuo Advanced Material Co., Ltd.
Powered by :www.300.cn Supported IPV6 Privacy Agreement